

This article follows the content creation and review process of A equipe de especialistas da Helian. Every figure is checked against our own test records before publication.
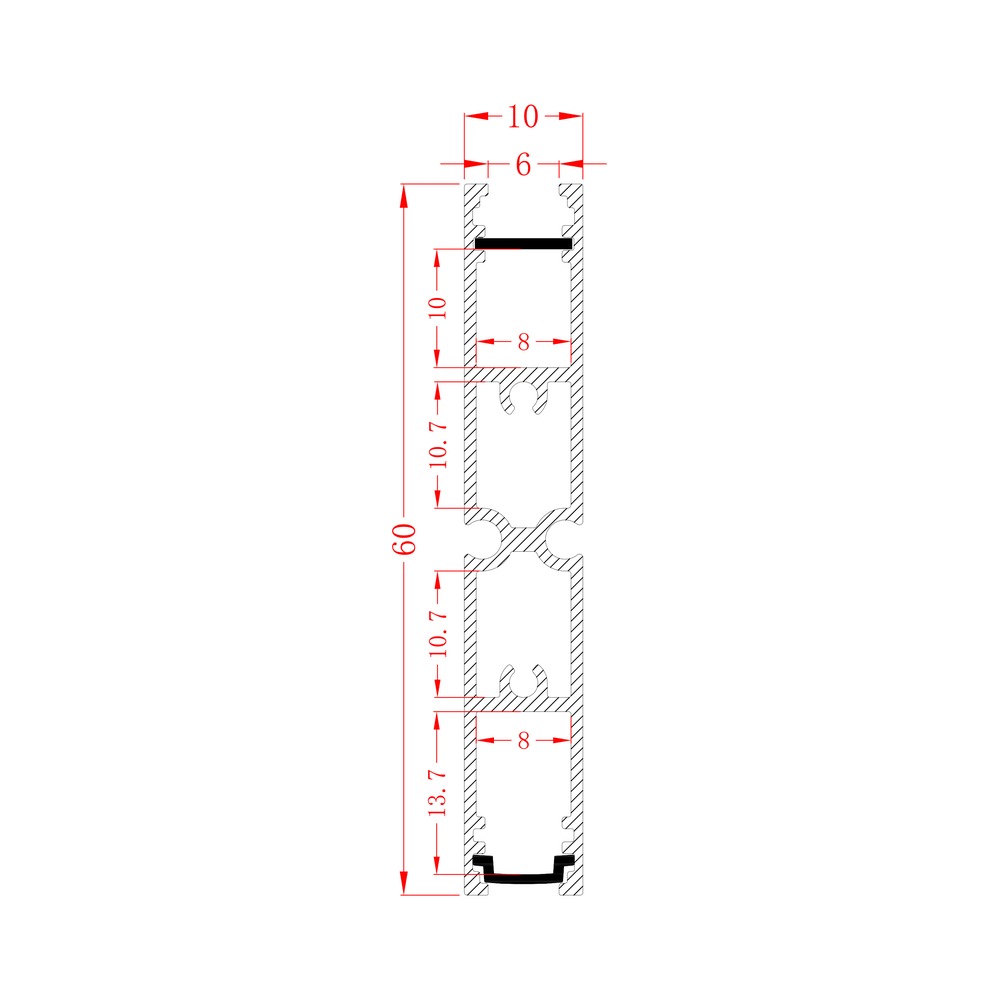
Cutting a 6063 extrusion is not difficult — a fine-toothed blade goes through it in seconds. The difficulty is in two places: keeping the cut square e deburring without touching the cover groove. A burr on the outside is cosmetic; a burr inside the groove means the diffuser will not seat, and no amount of force fixes it.
What tool cuts 6063-T5 cleanly?
Three tools work, in order of how clean the result is:
| Tool | Cut quality | Where it fits |
|---|---|---|
| Miter saw, non-ferrous blade | Cleanest, square repeatable | Workshop, runs with many pieces |
| Fine-toothed hacksaw | Good, needs a steady hand | One or two cuts on site |
| Jigsaw, metal blade | Rougher, more burr | Profile already fixed |
| Wood blade | Poor — grabs and wanders | Not for aluminum |
| Abrasive disc | Poor — heat and a burr along the whole edge | Not for a visible cut |
A miter saw with a non-ferrous blade. The cleanest and fastest for repeat cuts. The blade has a negative rake and a high tooth count, designed for aluminum rather than wood. This is what a workshop uses when a run has many pieces.
A fine-toothed hacksaw. Slower, but it works anywhere and needs no power. A 24-tooth blade or finer, with light pressure. This is the practical tool on site for one or two cuts.
A portable band saw or a jigsaw with a metal blade. Useful where the profile is already fixed and cannot be taken to a saw. The cut is rougher and needs more deburring.
What does not work well: a wood blade (the tooth geometry grabs and the cut wanders), an abrasive disc (it heats the metal and leaves a burr along the whole edge), and anything that cuts by crushing rather than by cutting.
Why does the blade matter more than the saw?
Because the cut quality is set by tooth geometry and feed, not by the machine.
Three things happen when a blade is wrong for aluminum:
- The teeth grab. A coarse wood tooth takes too big a bite, and the profile snatches — which is dangerous and also bends the section.
- The metal heats. A dull or inappropriate blade rubs rather than cuts, and 6063 softens as it warms. The cut then smears instead of shearing.
- The burr moves inside. A grabbing cut throws a burr on both faces, including the one you cannot see — the cover groove.
The practical rules: fine teeth, light feed, and let the blade cut rather than push it. A little paraffin or cutting fluid on the blade helps on long runs.
How do you deburr without damaging the groove?
Three steps, and the order matters.
1. File the outer faces first. Use a fine flat file, held at a shallow angle, working along the cut edge rather than across it. The aim is to remove the raised lip, not to chamfer the section.
2. Deburr the channel floor with a scraper, not a file. A file is wider than the groove and will round the internal corner, which is where the strip sits flat. A sharp scraper or the back of a blade, drawn along the floor, takes the burr off without touching the walls.
3. Check the cover groove with a fingernail. Run a nail along the groove on both sides. If it catches, the burr remains, and the diffuser will not seat. This takes five seconds and catches the fault that otherwise appears at assembly.
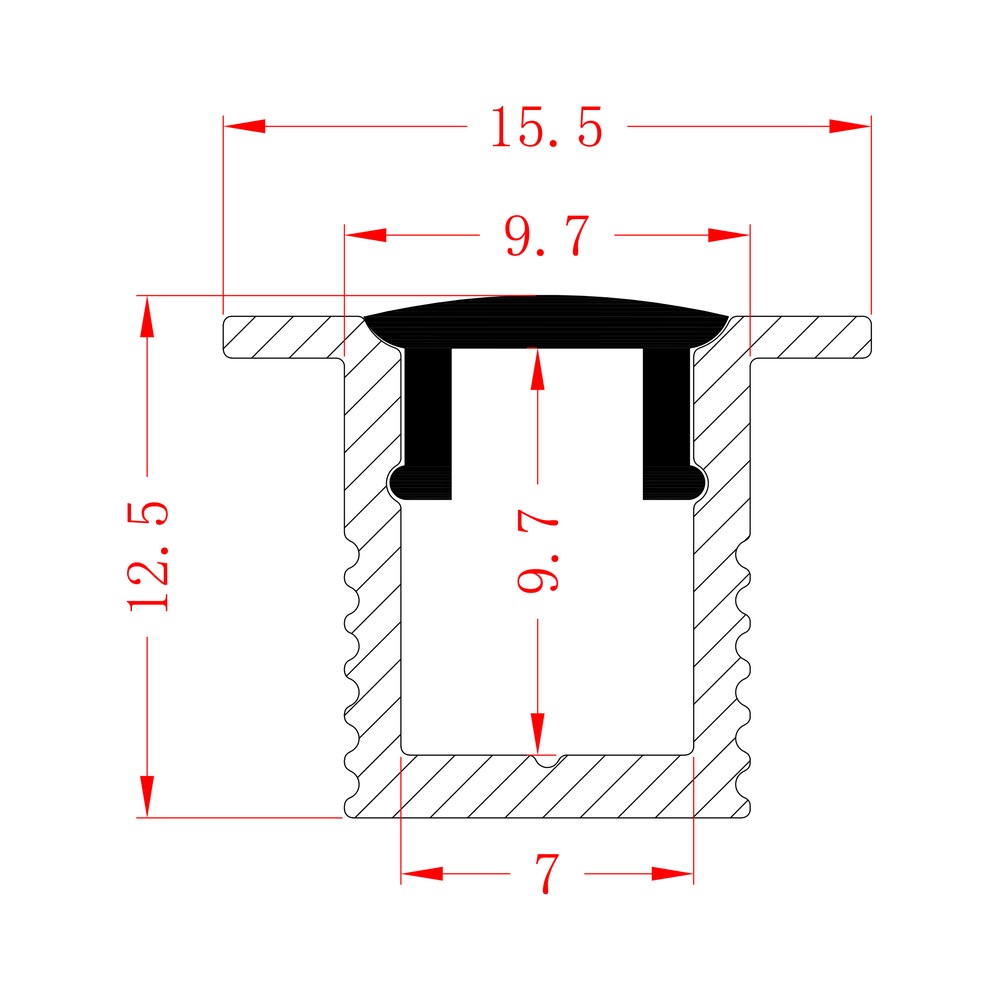
The one thing not to do: do not run a file across the aperture opening. The aperture edge is the visible line of the installation. A rounded or scratched aperture edge shows in the finished ceiling, and it cannot be repaired.
Where do you measure from?
From the channel, not from the end of the bar.
Two reasons:
- The bar end is not a reference. It may be cut at the factory, but it may also be a stock end that has been handled.
- What has to be right is the distance between features — the strip length between two joints, the aperture between two walls — not the overall length.
For a run that will be joined, measure between the joint faces, not between the outer ends. The connector takes up a fixed distance, and that distance is part of the run length, not extra.
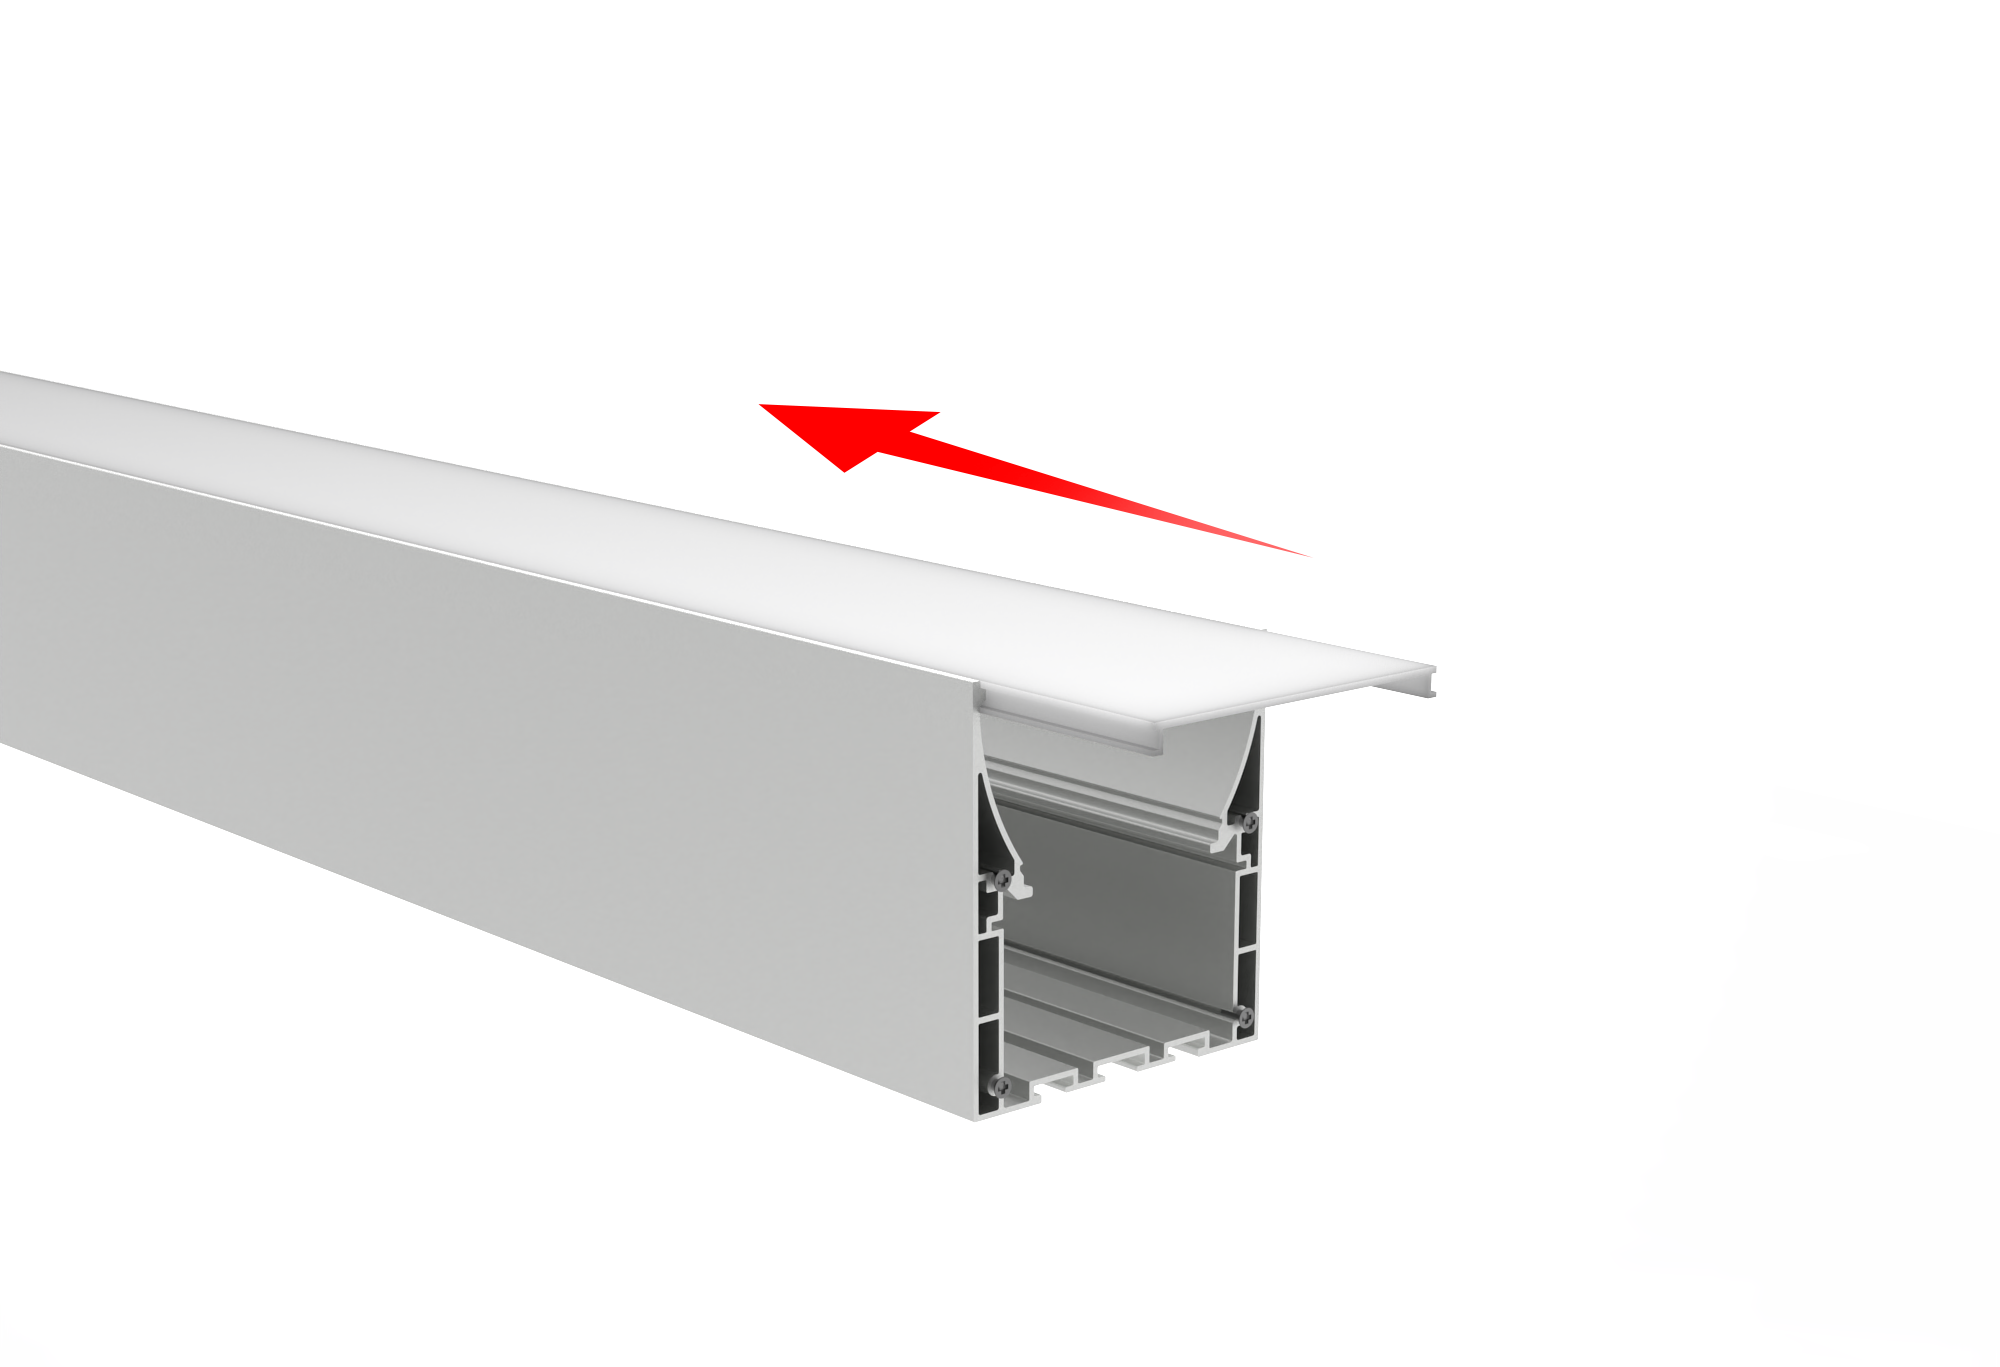
What about the cover and the strip?
Both are cut, and both are cut differently from the body.
The cover is cut with the same fine-toothed blade, but it is more brittle, and it scratches. Tape the cover before cutting, cut from the back face if it has one, and accept that the cut end will be visible unless an end cap covers it.
The strip is cut only at marked cut lines, and only with the power off. Between the cut lines there is a copper bus, and cutting outside them severs a section of the strip. The strip is also the item most often damaged during cutting — not by the blade, but by swarf.
Tape the aperture before cutting the body. This is the single most useful habit: a strip of tape over the opening stops aluminum swarf entering the channel. Swarf inside a channel is difficult to remove, and it defeats the adhesive when the strip goes in.
What length can you order?
Our profiles are supplied in any length up to 4 m, cut to your size. That is the figure to design around.
Two consequences for cutting:
- A run of 3.8 m is supplied as one piece. A run of 4.2 m is not — it needs a joint — which is a design decision, not a cutting one.
- Cutting shorter is normal; cutting longer is not possible. If a drawing calls for 4.5 m in one piece, the answer is a joint, a different section, or a different supply arrangement — not a longer bar.
For long runs, the useful approach is to set out the joints first, at changes of plane or at natural breaks, and then cut to those modules. A joint placed deliberately reads as a detail; the same joint in the middle of a straight line reads as a mistake.
What else goes wrong?
Four things, all avoidable:
Cutting without taping the aperture. Swarf in the channel, adhesive failure later.
Not checking square. A cut that is a degree out shows as a gap at the joint, and on a wide body it shows as a visible step.
Deburring the groove with a file. Rounds the internal corner, the strip no longer sits flat, and the thermal contact is lost.
Cutting the strip at the wrong point. The cut lines are marked; cutting between them destroys a section. On a run that needs an exact length, cut the body to suit the strip’s cut lines rather than the other way round.
Can I cut a profile with a wood chop saw?
Not with a wood blade. The same saw works with a non-ferrous blade. The difference is the tooth geometry and the rake angle, not the machine.
Do I need to deburr if the cut looks clean?
Yes. A cut that looks clean to the eye still has a raised lip along the edge, and that lip is what stops the cover from seating. Deburring is a minute’s work per end.
How do I cut a profile that is already fixed?
Use a jigsaw with a metal blade, or an oscillating tool, and work carefully to a marked line. Protect the surrounding surface, and expect to deburr more than you would on a bench cut.
Can I cut the diffuser shorter than the profile?
Yes, and often you should — a cover cut slightly short is easier to seat than one cut exactly to length, because the ends do not bind. The gap is hidden by the end cap.
What about cutting at an angle for a corner?
A miter cut needs both pieces cut at the same angle from the same reference, or the joint will not close. Cut one, check it against the other before cutting the second, and expect to deburr both faces of both pieces.