

Anodized vs Powder-Coated Aluminum: Which Finish Holds Up
Anodized or powder-coated? Film thickness, colour range, heat and slot tolerance decide it — and the coastal answer depends on sealing, not on the process name.
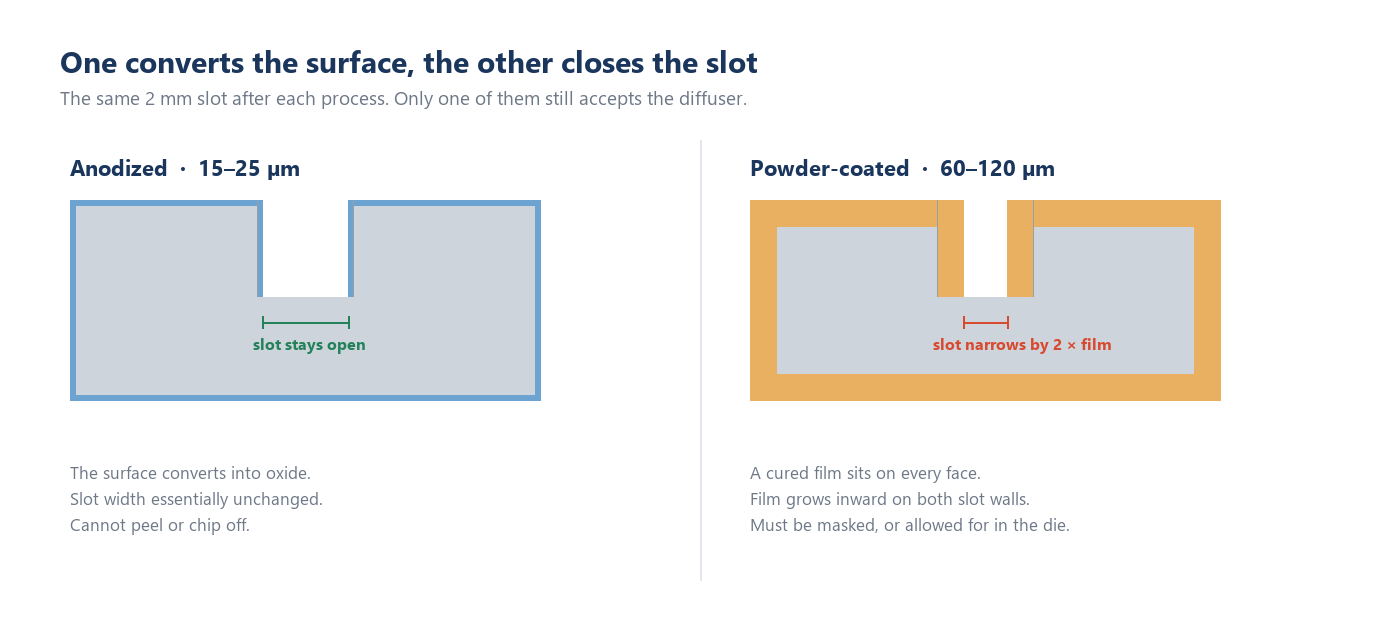
Neither finish is better in general. Anodizing converts the surface into a 15–25 µm oxide layer that cannot peel, holds a hard metallic look, and barely changes the dimensions. Powder coating lays down a 60–120 µm cured film in any RAL color, and swallows minor extrusion marks. The decision is film thickness against color range — plus one number most comparisons leave out: what the coating does to a 2 mm-wide diffuser slot.
What each process actually is
The two are not competing versions of the same thing. One modifies the metal, the other sits on top of it.
Anodizing is an electrochemical process. The aluminum is made the anode in an acid bath, and the surface converts into aluminum oxide — a hard, porous layer that is structurally part of the metal. The pores are then sealed, usually in hot water or a nickel-fluoride bath. That sealing step is what determines whether the finish survives outdoors.
Powder coating is electrostatic deposition. A dry resin powder is sprayed onto a grounded profile, then cured at roughly 180–200 °C so it melts, flows, and cross-links into a continuous film. There is no chemical bond to the metal — adhesion depends on pretreatment, and the film is thick enough to matter dimensionally.
| Property | Anodisé | Powder-coated |
|---|---|---|
| Film thickness | ~15–25 µm (typical) | ~60–120 µm (typical) |
| Bond to metal | Conversion of the surface itself | Adhesion after pretreatment |
| Scratch / wear | High — hard oxide, cannot peel | Moderate — chips at an impact point |
| Color range | Silver, black, bronze, champagne | Any RAL |
| Effect on dimensions | Negligible | Adds film thickness on all faces |
| Thermal path | Essentially unchanged | Reduced — the resin insulates |
| Typical outdoor life | 15–20 years when sealed | 5–8 years, UV-dependent |
The numbers above are typical published values across the finishing industry, not measurements from our line. They shift with alloy, bath chemistry, and powder grade, so treat them as a ranking.
The coastal disagreement
Search this topic and you will find two confident, opposite answers.
One group says anodizing is the coastal choice: harder, non-peeling, salt-spray tested, 15–20 years.
Another says anodizing fails faster at the coast: pitting within 12–18 months within 5 km of the shoreline, because the oxide layer is porous and chloride ions attack it, while a thick powder film is a continuous barrier.
Both are describing real failures, and neither is wrong about the mechanism. The variable they are omitting is sealing and film thickness.
An unsealed or thinly sealed anodic layer is a sponge. Sealed to spec — the oxide fully hydrated or nickel-fluoride sealed, thickness at the upper end of the range — it is a hard barrier that performs for decades. A powder coat applied over poor pretreatment will delaminate from the inside out no matter how thick it is.
So the useful question is not which process, it is:
What film thickness and what sealing does this supplier actually specify — and does it match the exposure?
If a quote says "anodized" with no thickness, it is not a specification. Ask for the micron figure and the sealing method, the same way you would ask for a wall thickness.
Where powder coating breaks the fit
This is the part that catches people on site, and it does not appear in finish comparisons.
A powder film adds 60–120 µm on every face — including the inside of the diffuser groove and the end-cap recess. Two consequences:
- The diffuser groove narrows. A groove designed with 0.2 mm clearance per side can end up too tight after coating, and a press-in cover will not seat without force.
- End caps and connectors no longer fit flush. The cap is sized to the extrusion, not to the extrusion plus film.
Experienced extruders mask critical faces before coating, or allow extra clearance in the die design. But not all do, and the failure shows up at assembly, not in the sample.
For a narrow section — say a 10 mm body with a 6 mm strip — the groove is a small fraction of the profile and the film is a large fraction of the clearance. On tight sections, anodizing is the lower-risk finish simply because it does not change the geometry.
Where powder coating is the only answer
Two cases where there is no real choice:
Trimless bodies. A trimless profile is filled and painted with the plaster. It has to take the wall color. Anodizing gives silver, black, bronze, or champagne — none of which match a painted wall. Powder coat in the specified RAL does, and it is the only way the line reads as a shadow gap rather than a metal strip.
Color-matched joinery. When the profile has to sit inside a lacquered cabinet or a specific ceiling color, the color range decides. Anodizing cannot match it.
There is a third, softer case: hiding extrusion marks. A powder film covers die lines and minor surface variation that anodizing exposes. On a long visible run, that difference is noticeable.
What we quote, and why it matters
Our specification sheet lists the finish as "Anodized / Painting" on 214 of 219 profiles, with 5 listed as anodized only. That slash is deliberate: it means the finish is specified per order, not defaulted.
That phrasing has a practical consequence for buyers:
- If you need a color match, say so at inquiry and give the RAL. The profile will be powder-coated.
- If you need coating-free geometry — a tight groove, a sliding fit, a snap-in cover on a small section — say so, and it will be anodized.
- If you say nothing, you will get whichever the factory is set up for that week, and it may not be the one your assembly needs.
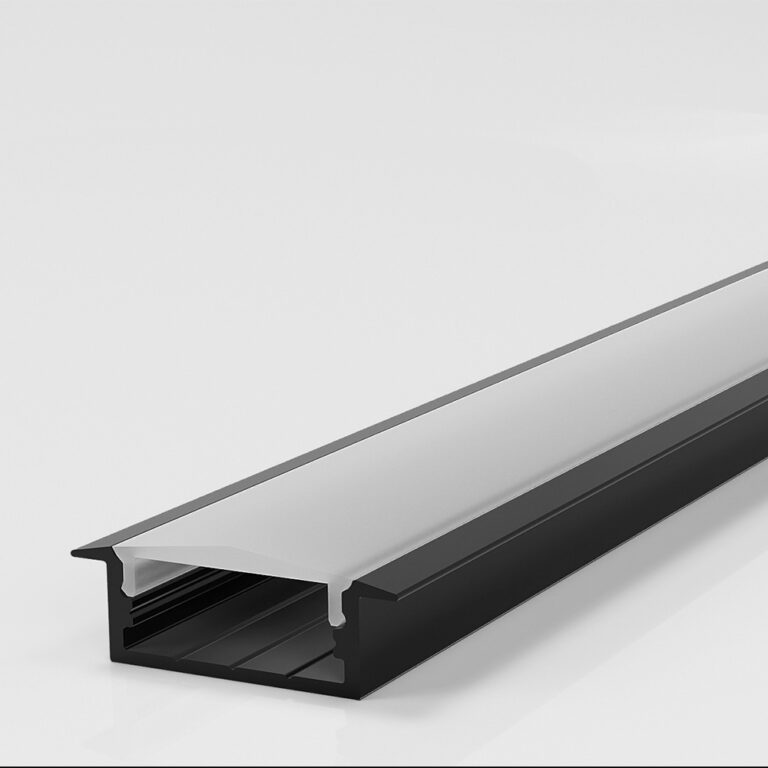
Ten profiles in the range are listed specifically as black anodized rather than the general "anodized / painting", because the black anodized look is the product — a matte black line against dark cabinetry or a shadow gap. Those are specified that way for appearance, not as a corrosion choice.
How to specify it in one line
Write the finish as a three-part requirement, not a single word:
Anodized, 15–20 µm, sealed — or powder-coated, RAL 9016, matte, 80 µm minimum.
Then add the one sentence that prevents the assembly problem:
Confirm that the diffuser groove and end-cap recess are either masked or sized to accommodate the film.
A supplier who can answer both is a supplier who has thought about the coating as a dimension rather than a color.
FAQ
Related links
We design and supply LED aluminum profiles and linear lighting — over 200 profiles with matched diffusers and fittings, serving customers in more than 100 countries since 2007.
Send the strip width, the run length and the destination — we will match the profile, the diffuser and the fittings, and quote within 1 business day.
Start your inquiry